Sulfur Recovery Unit Catalysts: Functions, Applications, and Loading Guide
Introduction
Sulfur recovery is a critical process in natural gas processing, oil refining, and petrochemical industries, where efficient conversion of sulfur compounds is essential for improving process efficiency, meeting environmental requirements, and ensuring reliable plant operation. In a sulfur recovery unit (SRU), catalyst performance has a direct impact on sulfur conversion, reactor efficiency, catalyst life, and overall process stability.
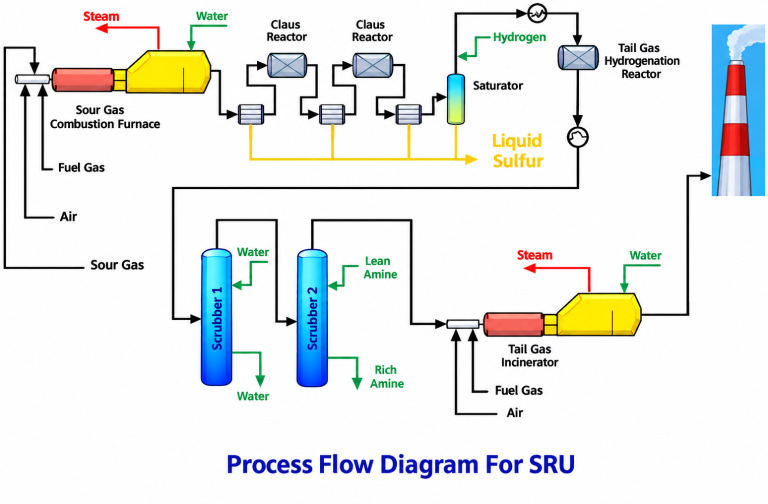
Because different reactions occur throughout the Claus process and tail gas treatment stages, a single catalyst cannot meet every operating requirement. Claus catalysts, hydrolysis catalysts, guard catalysts, and tail gas hydrogenation catalysts are designed to perform specific functions at different stages of the sulfur recovery process. Proper catalyst selection and loading are therefore important for achieving stable operation and maximizing sulfur recovery performance.
With more than 30 years of experience in catalyst and adsorbent technologies, CHEMPACK provides catalyst solutions for a wide range of industrial applications, including gas processing, oil refining, coal chemicals, and petrochemicals. Our technical approach focuses on matching catalyst properties and performance with specific process conditions and reactor requirements.
This article introduces the key functions and applications of different catalysts used in sulfur recovery units, followed by an overview of CHEMPACK’s PuriCat catalyst solutions for Claus reaction, COS and CS₂ hydrolysis, oxygen removal, and Claus tail gas hydrogenation.
- PuriCat PSR-1L high quality spherical activated alumina Claus catalyst for sulfur recovery unit in natural gas processing, oil refiners and other petrochemical industrials. It can be used in conventional Claus unit, as well as in sub-dewpoint units. PuriCat PSR-1L provides excellent catalytic activity for H2S/SO2 , COS and CS2 conversion due to its high surface area, high macroposity and thermal stability.
- PuriCat PSR-31E is extruded titanium dioxide Claus SRU catalyst, which is designed for hydrolysis COS and CS2 to H2S. PuriCat PSR-31E offers 95- 100% COS hydrolysis rate and 90-95% CS2 hydrolysis rate at reaction temperature of 280-340°C. Its excellent performance is due to a sophisticated manufacturing process and proprietary promoter.
- PuriCat PSR-31E can achieve long service life while maintaining high conversion due to superior resistance to sulfation and hydrothermal aging.
- PuriCat PSR-41 is iron promoted activated alumina sued as a guard layer in Claus reactors to remove oxygen from inlet process gas, protect Claus catalyst from sulfate formation. PuriCat PSR-41 offers typically installed in the 2nd and 3rd Claus reactors.
- PuriCat PSR-51TL is trilobe CoMo catalyst designed for Claus tail gas hydrogenation. PuriCat PSR-51TL offers high conversion of SO2 , COS, CS2 and CO due to optimized catalyst support.
Conclusion
The performance of a sulfur recovery unit depends on more than the basic Claus reaction. Different process stages require catalysts with specific catalytic functions, physical properties, and resistance to operating conditions. Selecting the appropriate catalyst for each reactor stage can help improve sulfur conversion, protect the catalyst bed, extend catalyst service life, and maintain stable SRU operation.
From Claus reaction and COS/CS₂ hydrolysis to oxygen removal and tail gas hydrogenation, each catalyst serves a specific purpose within the overall sulfur recovery process. Proper catalyst selection and loading should therefore be considered together with feed composition, reactor configuration, operating temperature, and process requirements.
CHEMPACK combines more than 30 years of experience in catalyst and adsorbent technologies with manufacturing capabilities and technical support to provide reliable solutions for demanding industrial applications. Our PuriCat catalyst series is designed to address different requirements across Claus sulfur recovery and tail gas treatment processes.
For refinery, natural gas processing, petrochemical, and other sulfur recovery applications, CHEMPACK works with customers to identify suitable catalyst solutions based on their specific process conditions and operational requirements. Through technology-driven solutions, reliable supply, and efficient technical communication, CHEMPACK is committed to supporting safer, more efficient, and more sustainable industrial operations.