
Popular Processes
Popular Products
With the increase of sulfur content in crude oil and natural gas and the tightening sulfur content in fuels, refiners and gas processers are pushed for efficient sulfur recovery capacities. At the same time, international environmental regulation agencies promulgate stringent standards for sulfur emission from oil, gas and chemical processing facilities. Chempack helps oil & gas companies to implement reliable, efficient and cost- effective technologies to cope with these changing requirements.
Chempack has the most extensive line of Claus Catalysts in the industry from one provider. In addition to non-promoted and promoted activated alumina catalysts, we offer titanium catalyst and active and inert bed supports. Chempack Claus Catalysts provide the quality needed for maximizing the performance of the SRU.
Chempack offers a wide portfolio of industrially proven, high-performance and top-conversion Sulfur Recovery Unit (SRU). They cover Claus units and Tail Gas Treatment Units (TGTUs) in oil refining and natural gas complexes, delivering the outstanding performance required by operators to succeed in these highly competitive industries.
1.Feed and Product:SRU combines acid gas and sour-water stripper gas to maximize sulfur recovery while meeting environmental emission standards.
2.Catalyst Function and Loading:CHEMPACK offers a complete Claus catalyst portfolio covering sulfur recovery, COS/CS₂ hydrolysis, oxygen removal, and tail-gas hydrogenation for reliable SRU performance.
3.Process Flow:The Claus process converts H₂S to elemental sulfur through thermal and catalytic stages, followed by tail-gas hydrogenation and amine absorption to maximize sulfur recovery and reduce emissions.
4. Production Specification:SRU main target is to recovery sulfur product on the premise of flue gas emission meeting the requirements of environmental protection.
5. Reference:So far, the technology has been used on over 40 commercial units.
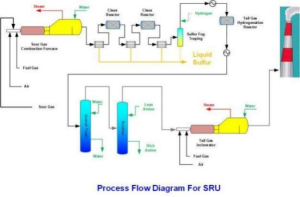
As sulfur content in crude oil and natural gas continues to increase and environmental requirements become more stringent, efficient and reliable sulfur recovery has become increasingly important for refineries, natural gas processing plants, and petrochemical facilities. A well-designed Sulfur Recovery Unit (SRU) must balance high sulfur recovery, stable operation, catalyst performance, and compliance with emission requirements.
CHEMPACK provides a comprehensive range of Claus catalysts and related solutions covering the key stages of sulfur recovery, including Claus reaction, COS/CS₂ hydrolysis, oxygen removal, tail-gas hydrogenation, and supporting materials. Combined with proven process technology and more than 30 years of experience in catalyst and adsorbent technologies, CHEMPACK helps customers optimize SRU performance, improve sulfur recovery efficiency, and maintain reliable long-term operation.
With the technology applied in more than 40 commercial units, CHEMPACK continues to provide reliable, efficient, and cost-effective sulfur recovery solutions for oil refining, natural gas processing, and other sulfur-containing gas treatment applications, supporting customers in meeting both operational and environmental requirements.

Copyright © Chempack.All rights reserved.